Machining cycle
Turning
The core roughing and finishing cycle for outer-diameter turning
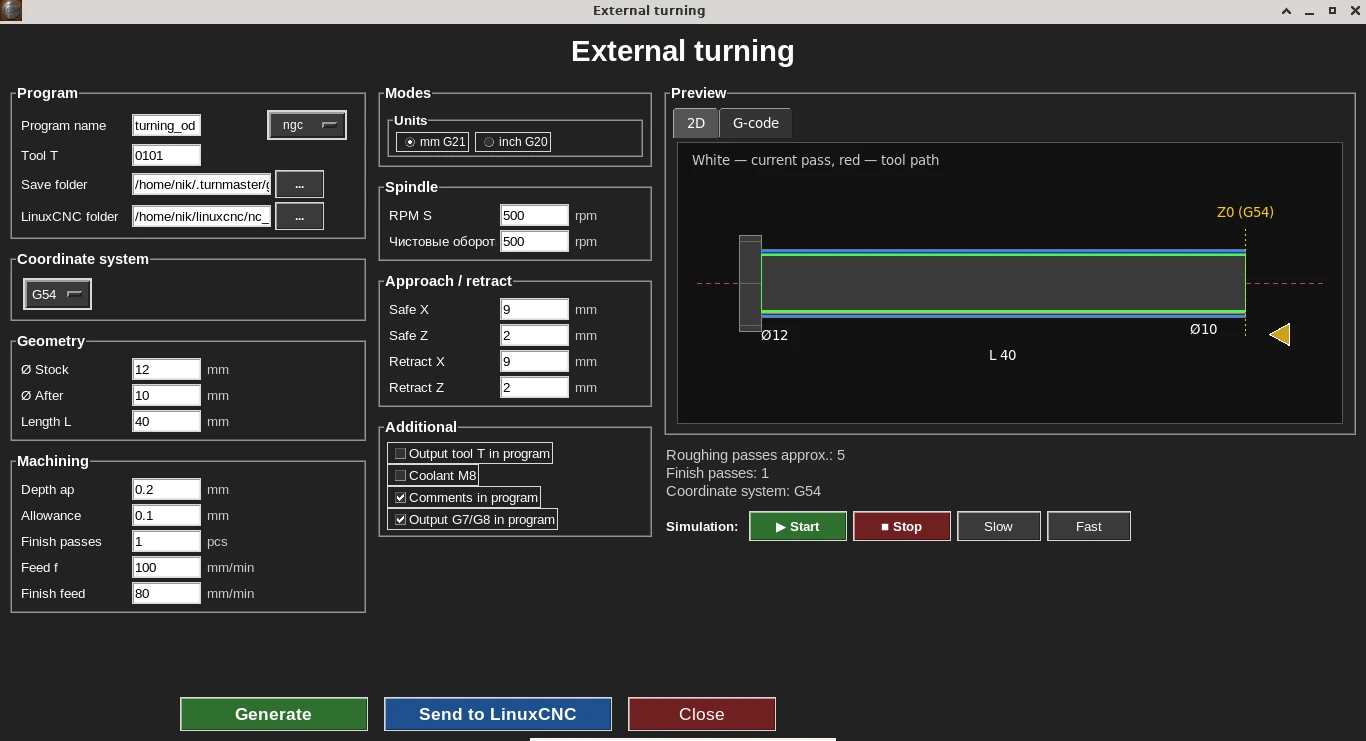
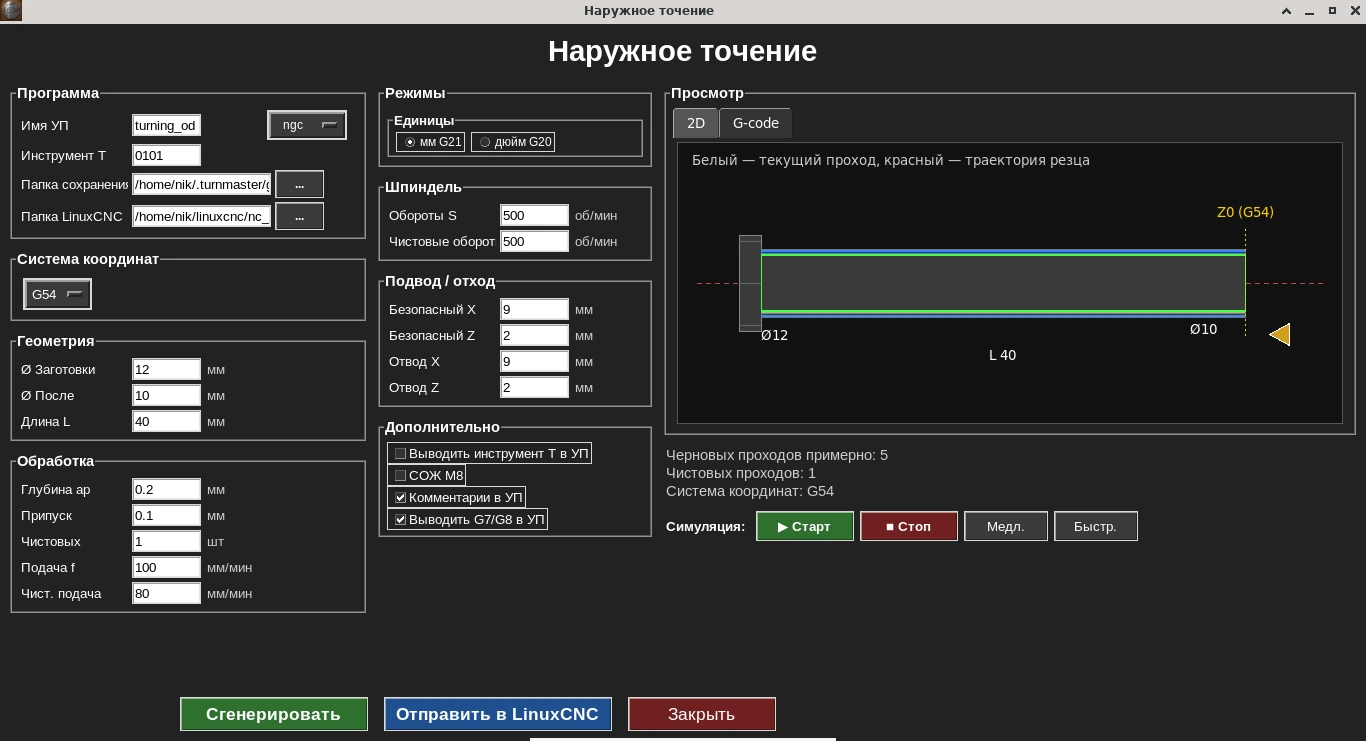
Cycle form: geometry, modes, and feeds on the left — live 2D toolpath simulator on the right, before generating G-code.
The turning cycle removes material down to the given diameters over one or several passes, automatically splitting the stock allowance between roughing and finishing passes.
Before generating G-code you can review the tool path in the live 2D simulator to confirm the passes are correct, and only then save the finished program for the machine.
Who needs this cycle
Needed in almost every turning job — from roughing a blank down to a finishing pass before the next operation.
Key form parameters
- •Start and end diameter
- •Length of the section
- •Finishing allowance
- •Feed rate (mm/rev or mm/min)
- •Spindle speed